English
O-Rings
O-Rings
O-Rings
O-Rings
O-Rings
O-Rings
O-Rings
O-Rings
O-Rings
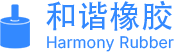
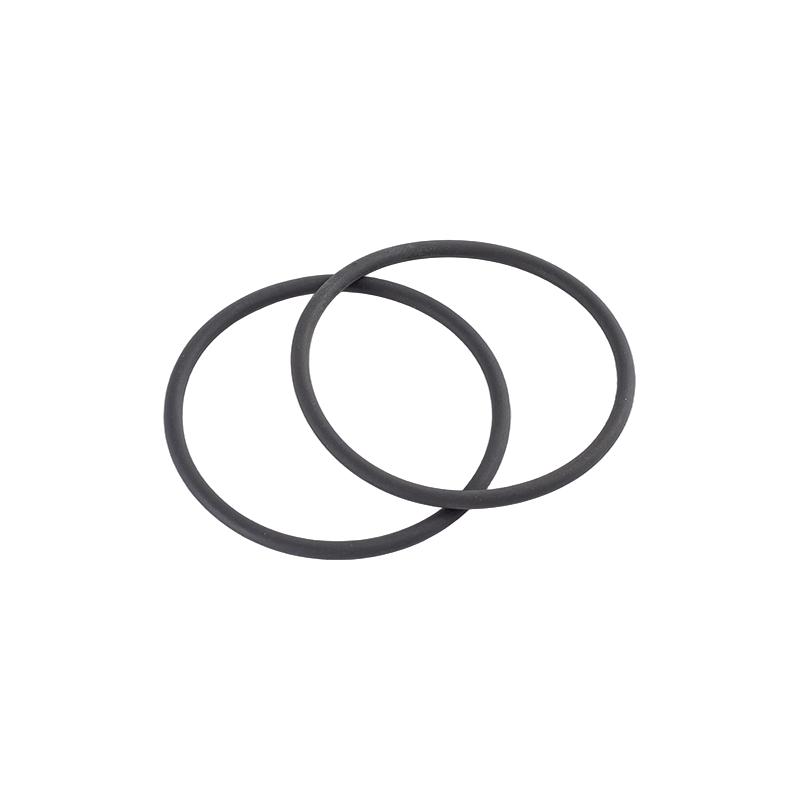
Silicone O-Rings (VMQ)
Silicone O-Rings (VMQ) are made from food-grade silicone rubber and molded in a clean-room environment. They are non-toxic, odorless, and resistant to aging, and can come into direct contact with food and liquid medicine without releasing harmful substances, meeting relevant food-contact and medical hygiene standards.
Contact Us
- Product Details
- Contact Us
This product offers excellent high- and low-temperature resistance, withstanding temperature changes from -60°C to 200°C. Even after repeated high-temperature steam sterilization or switching between refrigerated environments, it retains its elasticity without aging or hardening. The product supports customization in transparent, white, and various other colors, making it easy to distinguish equipment appearance and identify according to industry standards.
Silicone O-Rings are widely used for interface sealing in food processing machinery, medical device tubing connections, and leak-proof structures inside bathroom faucets and shower heads, and are also suitable for high-temperature conditions such as ovens and steaming equipment, making them a common sealing choice for food and medical industry equipment with high requirements for material safety and high-temperature sterilization resistance.
This product can be supplied with material inspection reports that meet relevant food-contact standards and supports sample confirmation based on customer drawings or samples, meeting selection needs for different sealing pressures and installation spaces.
Hot products
Company
Taizhou Hexie Rubber Co., Ltd.
Taizhou Hexie Rubber Co., Ltd. specializes in the R&D and manufacturing of industrial sealing products, anti‑vibration components and custom silicone rubber products, offering both standard parts and non‑standard customization services. Our product portfolio includes various rubber seals, metal sealing rings, oil seals, hydraulic & pneumatic seals, high‑performance specialty seals, rubber vibration dampers, molded and extruded silicone goods. Materials such as NBR, FKM, EPDM, silicone, PTFE and FFKM are available for selection. Serving machinery, automotive, automation, food‑medical, new‑energy and other industries, we deliver reliable solutions for diverse complex working conditions with professional product selection and custom processing capabilities.
Latest News
Contact
-
 3839567060@qq.com
-
 +86 138 6769 2238
-
 No. 80, Zhangzi Road, Zhang'an Street, Jiaojiang District, Taizhou City, Zhejiang Province, China (8 rooms on the first floor)
QR Code
Copyright © Taizhou Hexie Rubber Co., Ltd. All Rights Reserved